

Equipment
Barre latérale
Transformation Equipment and Methods


 Thermo Scientific™ iCAP™ 7000 ICP-OES System


 Particle size analyzer


 Parr 6050 Compensated Jacket Calorimeter

 GENESYS™ 50 UV-Visible Spectrophotometer


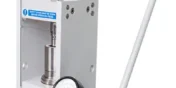 Specac hydraulic press

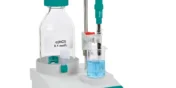 916 Ti Touch titrator

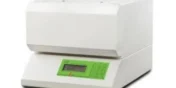 FOX 600 Heat Flow Meter
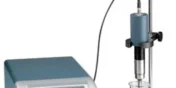 Ultrasonic Processor (Sonicator S-4000)

200 L Inconel Reactor with Oil Heating and Cooling
The 200 L Inconel C22 reactor, manufactured by NanoMag, is a high-pressure pilot-scale reactor designed for advanced chemical and biorefinery applications. Constructed from corrosion-resistant Inconel C22, the system is particularly well suited for demanding reaction environments involving aggressive chemicals, elevated temperatures, and high pressures.
Key Features
- NanoMag Inconel C22 reactor
- Maximum working volume: 130 L
- Maximum operating pressure: 60 bar
- Maximum operating temperature: 200°C
- Oil-heated and oil-cooled jacketed system for precise thermal control
- Corrosion-resistant construction for harsh processing conditions
- Suitable for pilot-scale process development and scale-up
Typical Applications
- Scale-up of novel chemical processes for the liquefaction of lignocellulosic biomass
- Optimization of lignin recovery processes
- Biorefinery process development and validation
- Organosolv pulping processes
- Levulinic acid production
- Pilot-scale conversion of biomass into value-added chemicals and bio-based products
- Research and development of sustainable and circular bioeconomy technologies

200 L Inconel Reactor with Electric Heating
The 200 L Inconel C22 reactor, manufactured by NanoMag, is a versatile pilot-scale processing system designed for operation under demanding chemical reaction conditions. Constructed from highly corrosion-resistant Inconel C22, the reactor is suitable for handling aggressive chemicals and challenging process environments while providing reliable temperature and pressure control.
Key Features
- NanoMag Inconel C22 reactor
- Maximum operating pressure: 20 bar
- Maximum operating temperature: 250°C
- Electric heating system with integrated heating elements
- Internal water-cooling coil for process cooling
- Equipped with an agitator for efficient mixing
- Excellent resistance to corrosive chemicals and harsh operating conditions
- Designed for pilot-scale process development and scale-up
Typical Applications
- Scale-up of innovative chemical processes for lignocellulosic biomass liquefaction
- Optimization of lignin recovery and valorization processes
- Biorefinery process development and demonstration
- Organosolv pretreatment and fractionation processes
- Levulinic acid production and biomass conversion pathways
- Development of sustainable bio-based chemicals and materials
- Pilot-scale testing of advanced chemical and thermochemical processes
Integrated Reactor Platform
The two NanoMag Inconel C22 reactors offer complementary operating capabilities, enabling a wide range of pilot-scale process development activities. Their robust construction, integrated agitation systems, and resistance to aggressive chemicals make them ideal tools for biomass processing, biorefinery applications, chemical synthesis, and process scale-up studies.
Pre-Commercial Supercritical Extraction Unit
The pre-commercial supercritical fluid extraction (SFE) unit, manufactured by Separex, is designed for process scale-up, pilot production, and market validation of high-value natural products. The system can process up to 50 L of raw material using supercritical CO₂, a sustainable and environmentally friendly solvent recognized for its efficiency and selectivity.
Key Features
- Separex pre-commercial supercritical extraction unit
- Processing capacity of up to 50 L of raw material
- Maximum operating pressure: 700 bar
- Operating temperature range: 35°C to 100°C
- Uses supercritical CO₂ as a green solvent
- Suitable for process scale-up and pilot production
- High selectivity and product purity
- Reduced solvent residues and environmentally friendly operation
Typical Applications
- Extraction of active compounds from cannabis
- Coffee decaffeination
- Recovery of flavors and aromas from fruits, plants, and seeds
- Extraction of oils from plant and marine biomass
- Production of high-value natural ingredients for food, nutraceutical, cosmetic, and pharmaceutical applications
- Scale-up and pre-commercial validation of extraction processes

High-Pressure Reactors (3 L and 6 L)
Applications
- High-pressure chemical synthesis
- Liquid-phase process development
- Catalytic reactions
- Biomass valorization
- Chemical conversion processes
- Feasibility and scale-up studies
- Research involving corrosive or demanding operating conditions

Pilot-Scale Spray Dryer
This pilot-scale spray drying unit is designed for the processing of significant volumes of aqueous solutions and suspensions. It offers a maximum evaporation capacity of up to 6 kg/h, depending on inlet and outlet temperatures as well as other operating conditions.
Operating Parameters
- Maximum inlet temperature: 350°C
- Maximum outlet temperature: 120°C
- Process air flow at 200°C: 80 kg/h
- Atomization system: Rotary atomizer
Typical Applications
- Production of pilot-scale powder batches
- Drying of oat milk, chicken broth, proteins, and bark extracts
- Scale-up studies for bioplastic drying processes, including PHA (Polyhydroxyalkanoates)
- Development and optimization of spray drying processes for food, bio-based, and specialty products

100 L Bioreactor
The 100 L bioreactor, manufactured by LEE Industries Inc., is designed for the scale-up of microbial fermentation and bioprocessing applications. Suitable for both batch and continuous operation modes, this pilot-scale unit provides a controlled environment for process development, optimization, and technology transfer.
Key Features
- 100 L pilot-scale bioreactor
- Manufactured by LEE Industries Inc.
- Suitable for batch and continuous fermentation
- Double-jacketed stainless-steel vessel
- Maximum operating pressure: 2 bar
- Maximum operating temperature: 150°C
- Designed for microbial and enzymatic process scale-up
- Robust and sanitary construction for bioprocess applications
Typical Applications
- Scale-up of microbial fermentation processes
- Development and optimization of biotechnological production systems
- Scale-up of enzyme-based bioprocesses
- Production of bio-based compounds, metabolites, and bioproducts
- Process validation and pilot-scale biomanufacturing
- Research and development in industrial biotechnology

100 L Filter-Bottom Reactor
The 100 L jacketed filter-bottom reactor, manufactured by ACE Glass Corporation, is a versatile pilot-scale system designed for reaction, filtration, and drying operations within a single unit. Its multifunctional design makes it particularly suitable for process development, extraction, purification, and product recovery applications.
Key Features
- 100 L jacketed filter-bottom reactor
- Manufactured by ACE Glass Corporation
- Heating capability up to 120°C
- Efficient agitation for homogeneous reaction conditions
- Cooling capability to ambient temperature
- Integrated filtration and product recovery system
- In situ drying of filtered solids up to 120°C
- Nitrogen sparging system for inert atmosphere operation
- Suitable for reaction, filtration, and drying in a single vessel
Typical Applications
- Extraction of polyphenols from bark, fruits, and other plant materials
- Production and purification of natural extracts and bioactive compounds
- Pilot-scale chemical and biochemical processing
- Solid-liquid separation following synthesis or extraction processes
- Product isolation, drying, and recovery in a single integrated unit
- Process development and scale-up for nutraceutical, pharmaceutical, and specialty chemical applications

100 L Reflux Distillation Column
The 100 L reflux distillation column, manufactured by Ablaze, is an essential pilot-scale system for large-scale distillation processes, combining capacity, efficiency, and operational versatility. The unit is designed for the separation, purification, and recovery of chemical products across a broad range of industrial applications.
Key Features
- 100 L reflux distillation column
- Manufactured by Ablaze
- Working volume: 60 L
- Maximum operating temperature: 180°C
- Maximum operating pressure: 0.5 bar
- Suitable for batch distillation and product purification
- Efficient solvent recovery and recycling
- Designed for pilot-scale process development and scale-up
Typical Applications
- Fractionation and separation of chemical compounds
- Product purification and solvent recovery
- Separation of complex mixtures in fine chemistry and specialty chemical production
- Process development and optimization for distillation operations
- Recovery and recycling of organic solvents
- Pilot-scale validation of purification and separation processes

200 L Nutsche Filtration Unit
The 200 L pilot-scale Nutsche filtration unit, manufactured by Ablaze Glass, is designed for the processing of a wide range of synthetic and natural products in a fully enclosed system. The unit operates under conditions ranging from full vacuum to 0.5 bar pressure, providing flexibility for various filtration and solid-liquid separation processes.
Key Features
- 200 L pilot-scale Nutsche filtration unit
- Fully enclosed filtration system
- Operating pressure range: full vacuum to 0.5 bar
- Operating temperature range: -20°C to 180°C
- Interchangeable filter media with pore sizes from 50 to 22 μm
- Compatible with pilot-scale reactor systems
- Suitable for solid-liquid separation, clarification, and product recovery
Typical Applications
- Downstream processing for 200 L pilot-scale reactors
- Filtration of nutraceutical extracts, including polyphenols, fruit extracts, and other bioactive compounds
- Separation of solid particles from chemical synthesis products and distillates
- Removal of suspended solids from industrial wastewater streams
- Clarification of botanical and plant extracts
- Clarification of microbial culture media for the retention of microorganisms and suspended matter
- Product recovery and purification in chemical, biotechnology, and natural product processing

200 L Decantation Unit
The 200 L decantation unit, manufactured by Ablaze Glass, provides a versatile and efficient solution for liquid-liquid phase separation across a wide range of industrial applications.
Key Features
- 200 L decantation unit
- Up to 180 L working volume
- Vacuum operation capability
- Operating temperature range: -20°C to 180°C
- Corrosion-resistant construction
- Suitable for pilot-scale process development and scale-up
Typical Applications
- Downstream processing unit for 200 L reactors
- Scale-up of liquid-liquid separation processes from chemical or biological reactors
- Separation of immiscible liquid phases following reaction or extraction processes
- Removal of suspended solids and organic matter from wastewater streams
- Process development and optimization for industrial separation operations

Semi-pilot scale bioreactor
Labfors 5 TM is an easy-to-use bench-top bioreactor. Different culture strategies such as batch culture, fed-batch and continuous modes could be applied. The touch screen provides precise and reliable control and communication with the IRIS supervision software. CÉPROCQ has a reactor with two interchangeable tanks with a capacity of 3.6 L and 7.5 L with working volumes of 2.3 L and 5 L.

20 L Rotary Evaporators
Key Features
- Two pilot-scale Büchi R-220 rotary evaporators
- 20 L flask capacity
- PTFE sealing system for enhanced thermostability and chemical resistance
- Dual heating mode: water bath or oil bath
- Integrated overheating protection
- Suitable for solvent recovery, concentration, and drying applications
Typical Applications
- Scale-up of rotary evaporation processes for extracts obtained with various organic solvents
- Production of small pilot batches of dried extracts
- Solvent removal and concentration of natural products, bioactive compounds, and specialty ingredients
- Process development and optimization for extraction and purification workflows

Pilot-Scale Supercritical Extraction Unit
The pilot-scale supercritical extraction unit, manufactured by Separex, is designed for the extraction of high-value compounds from a wide range of natural feedstocks using supercritical CO₂, an environmentally friendly and sustainable solvent.
Key Features
- Separex pilot-scale supercritical extraction unit
- Processing capacity: 4 L
- Maximum operating pressure: 300 bar
- Maximum operating temperature: 100°C
- Uses supercritical CO₂ as a green solvent
- Suitable for heat-sensitive compounds
- High selectivity and extract purity
- Supports process development and scale-up studies
Typical Applications
- Extraction of cannabinoids and other bioactive compounds from cannabis
- Coffee decaffeination
- Extraction of hop aromas and flavor compounds for the brewing industry
- Extraction of natural vanilla flavor compounds
- Recovery of polyphenols and antioxidant molecules
- Processing of lignocellulosic biomass for biobutanol production
- Extraction of oils from plant, algal, and microbial biomass
- Development of sustainable extraction processes for food, nutraceutical, cosmetic, and biotechnology sectors

Pilot unit for subcritical water extraction
The pilot unit of subcritical water extraction has been fabricated at CEPROCQ. This type of extraction takes place at temperatures between the boiling point and the critical point of water (374.1 ° C, 221 bar), with enough pressure to keep the water in the liquid state and allow to extract polar and less polar compounds. This technique is emerging as a promising and powerful alternative to conventional techniques and is a breakthrough in finding alternatives to organic solvents.

Liquid-liquid extraction pilot unit
In most bioindustrial processes, the raw materials must be treated to obtain a pure extract with the desired properties. The liquid-liquid extraction pilot unit with a Karr™ agitated column allows to treat 20 liters of liquid extract.

Pilot unit of membrane extraction
The hollow fiber membrane contactor makes it possible to extract and concentrate metal ions and organic molecules by liquid-liquid extraction, or inorganic molecules like ammonia by liquid-gas-liquid extraction. The unity of CEPROCQ can treat 60 liters / hour of effluent. However, its capacity can be increased by using larger contactors. The basic treatment unit includes two tanks, two peristaltic pumps and one contactor, which can be assembled quickly on site to evaluate its potential.

Pilot unit for advanced oxidation (AOP)
To treat industrial and agricultural wastewater, CÉPROCQ uses advanced oxidation technologies (ozone, hydrogen peroxide, ultraviolet). Creating highly oxidizing entities (such as hydroxyl radicals) allows destruction of a wide range of nonbiodegradable organic compounds. An in-house fabricated pilot unit facilitates applying these three oxidants separately or in combinations for treatment of wastewater. The unit could be used for treatment of 10 to 30 litres wastewater.

Multi-Zone Tube Furnace (TFM Series)
The TFM Series Multi-Zone Tube Furnace, distributed by Across International, is an advanced thermal processing system designed for precise temperature-controlled applications in research, development, and pilot-scale production environments.
Key Features
- TFM Series Multi-Zone Tube Furnace
- Distributed by Across International
- Multi-zone temperature control for precise thermal profiling
- Suitable for continuous and batch processing
- Easy operation and process control
- Uniform temperature distribution
- Designed for research, development, scale-up, and material characterization
- Compatible with a wide range of process atmospheres and materials
Typical Applications
- Thermal treatment of advanced materials
- Metallurgical processing and heat treatment
- Glass and ceramic material development
- Synthesis and processing of lithium-ion battery anode and cathode materials
- Development of new energy materials and technologies
- Calcination, pyrolysis, and carbonization processes
- Material characterization under controlled temperature conditions
- Pilot-scale process development and optimization

Laboratory scale spray dryer
Spray drying is a dehydration technology for suspended or dissolved materials. Unlike the traditional drying in an oven, through spray drying, the sample spends only a few seconds (1 - 1.5 sec) in a high temperature zone. Therefore, it is highly recommended for drying temperature-sensitive materials (e.g. antioxidants). CÉPROCQ has a laboratory scale spray dryer unit: Buchi Mini Spray Dryer B-290™. It is a laboratory equipment capable of drying up to 30 ml/min of an aqueous solution. The output particle size could be adjusted between 2 and 25 μm.

Freeze-drying at pilot scale
Freeze-drying (lyophilization) is a method of removing water by sublimation of the ice crystals from the frozen material. The process allows a better-quality products, compared to products dried with traditional methods. CÉPROCQ has a pilot freeze dryer: VirTis Genesis 35LTM pilot freeze dryer. It is designed to meet all the requirements of freeze drying, such as storage temperature as low as -70 ° C and condenser temperature up to -85 ° C. It has 4 shelves that can accept trays of 3 L each. The unit is equipped with a control system and temperature and vacuum sensors, in order to configure the conditions of freeze-drying, according to the requirements of the application.

Gas chromatography
Gas chromatography (GC) is a very effective technique for analyzing volatile and non-labile molecules in liquids and gases. The gas chromatograph coupled with a mass spectrometer (GC-MS) could be used to identify unknown molecules using a database containing more than 267,000 compounds. This technique could determine the composition of products obtained from biorefining, catalytic processes, pyrolysis. In addition, a special database has been added to quickly determine the composition of any essential oil. A whole range of injectors and detectors are available to analyze many different samples. various injection including split / splitless, on column, Solid Phase Micro Extraction (SPME) injections could be performed. The unit is also equipped with a gas injector. Specific detectors such as NPD, ECD, FPD can be also installed. The flame ionization detector (FID) is mainly used to quantify catalysis products, food extracts or solvents and the thermal conductivity detector is used to quantify gases ranging from simple gases such as CO2 or methane to more complex gases.

High performance liquid chromatography (HPLC)
High performance liquid chromatography (HPLC) is an analytical technique used to separate molecules from a complex mixture in a column. Once the molecules have been separated, they enter a detector. To quantify molecules, this device has conventional detectors such as a UV-Visible spectrometer (DAD diode Array detector), a fluorescence detector as well as refractive index detectors (RID). By applying these detectors, a wide range of molecules such as sugars, pharmaceutical molecules, polyphenols could be quantified. Moreover, the size of molecules, such as lignin could be determined.

HPLC Q-TOF
The Q-TOF detector can identify and quantify molecules at very low concentration, as well as unknown molecules.
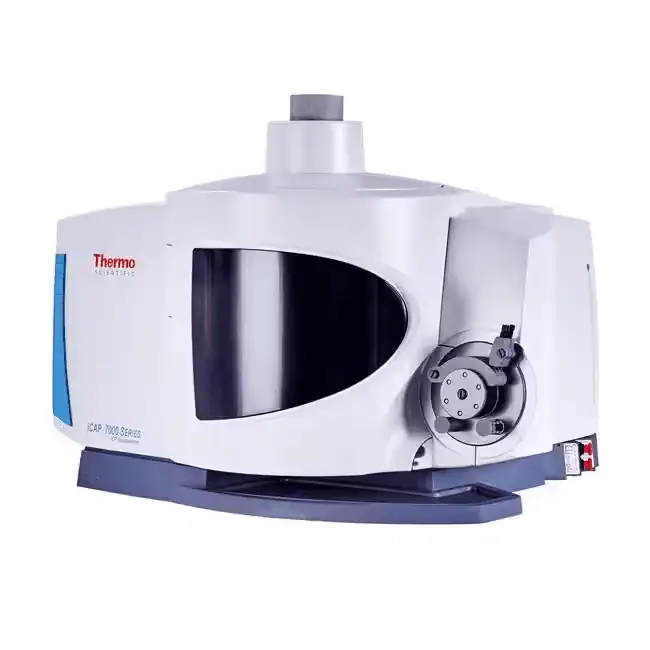
Thermo Scientific™ iCAP™ 7000 ICP-OES System
The Thermo Scientific™ iCAP™ 7000 ICP-OES System is an advanced solution in inductively coupled plasma optical emission spectrometry, combining high analytical performance with cost-effective operation. Ideal for laboratories seeking speed, reliability, and precision, it meets the highest standards in elemental analysis. Advantages:
- Fast, simultaneous multi-element analysis with an echelle grating polychromator, delivering high-resolution spectra and broad spectral coverage from 167.4 to 847.0 nm.
- Thermal stability ensured by ±0.1 °C thermostatic control, guaranteeing consistent results even during prolonged analyses.
- Advanced optical design with an optimized purge system and a sealed optical path, reducing interferences and minimizing maintenance costs.
- Compact and intelligent design that minimizes footprint while maximizing optical performance.
- Environmental analysis,
- Agriculture,
- Pharmaceuticals,
- Mining industry,
- Petrochemicals,
- Industrial quality control.

Vario MACRO cube Elemental Analyzer
The vario MACRO cube by Elementar is a high-performance elemental analyzer designed for the simultaneous determination of carbon (C), hydrogen (H), nitrogen (N), oxygen (O) and sulfur (S) in a wide range of solid, liquid, and viscous samples. Capable of analyzing macro-sized samples up to 1.5 g, it delivers accurate and reliable results while minimizing sample preparation requirements. Its versatility and automation make it an ideal solution for the analysis of soils, biomass, fossil fuels, petroleum products, and environmental materials.

Specific surface area (BET) and porosity analyzer
The Micrometrics Tristar II analyzer™ is used for determination of specific surface area of solids and porous materials such as biochar or lignin. Moreover, it could be used to measure the total pore volume and the pore size distribution of a solid sample. The analyzer works with both CO2 and N2 isotherms. In addition, the analyzer is equipped with a three-station degasser, which allows the user to degas 3 samples at the same time. Three analysis stations allow the operator to perform a triplicate analysis in one step.
| Parameter | Detection limit |
| Specific surface (m2/g) | ≥ 0,01 |
| Total area surface (m2) | ≥ 0,1 |
| Pore volume (cm3/g) | ≥ 4×10⁻⁶ |
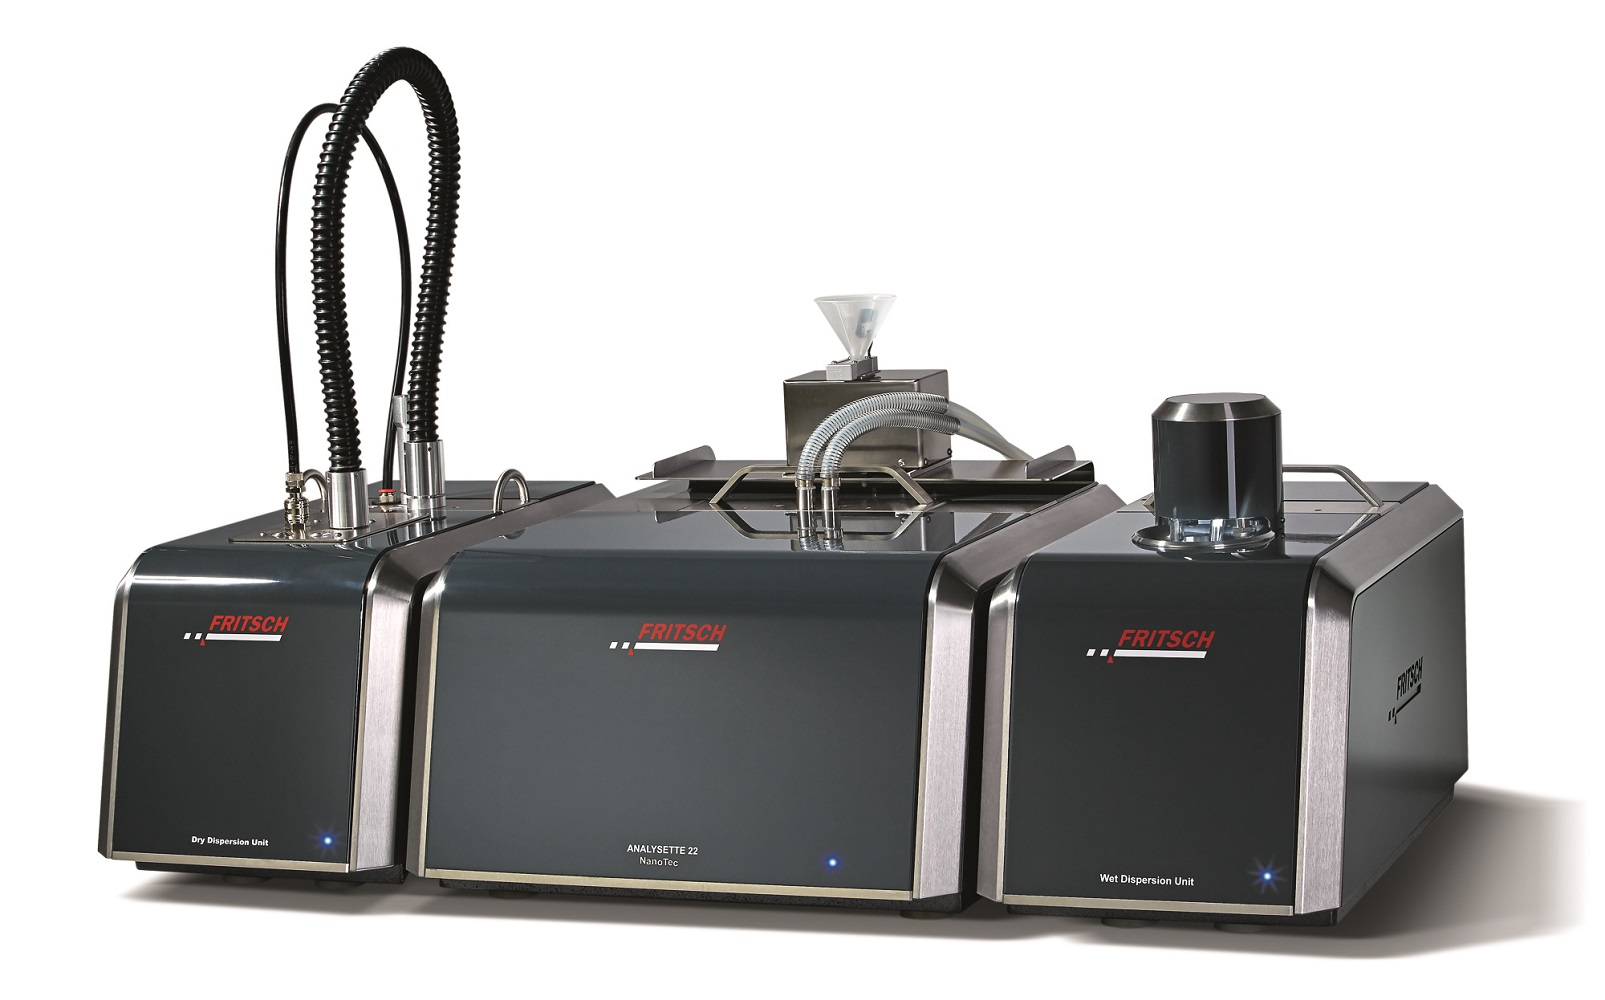
Particle size analyzer
It is a FRITSCH Nanotec™ particle size analyzer by laser light scattering technology. The wet and dry mode allow us to measure the particle size distribution of a solid and a suspension. The measuring range is 0.01 to 2100 μm for suspension and 0.1 to 2100 μm in dry mode.

Total carbon analyzer
The TOC analysis shows the total amount of organic carbon in municipal wastewater, industrial wastewater, and process water. This analysis is generally used to know the rate of pollution of a water or to monitor the effectiveness of its treatment. TOC measurement is based on: 1) the oxidation of organic carbon to carbon dioxide, and 2) the measurement of carbon dioxide generated by infrared. Ability to measure Total Carbon (TC), Inorganic Carbon (IC), and Total organic Carbon (TOC, by TC-IC difference) and Total Nitrogen (TNb). Range from 4 μg / l to 30,000 mg /l (Shimadzu TOC-L Series device™).

FTIR (Fourier Transform Infrared Spectroscopy)
FTIR can characterize a solid or liquid product (Nicolet iS50 FTIR™ device) . It is a non-destructive technique, which does not require sample preparation, except grinding for solids samples. The resulting spectrum reflects the molecular vibrations under the light effect as a function of wavelength. The results are the peaks related to functions of the molecule such as OH, CH, C = O, COO-, C = C, C≡C, C≡N, NH, NH2, etc. This technique makes it possible to characterize organic compounds as well as inorganic ones. Although it is a qualitative method, it can be used for quantitative measurement under certain conditions.
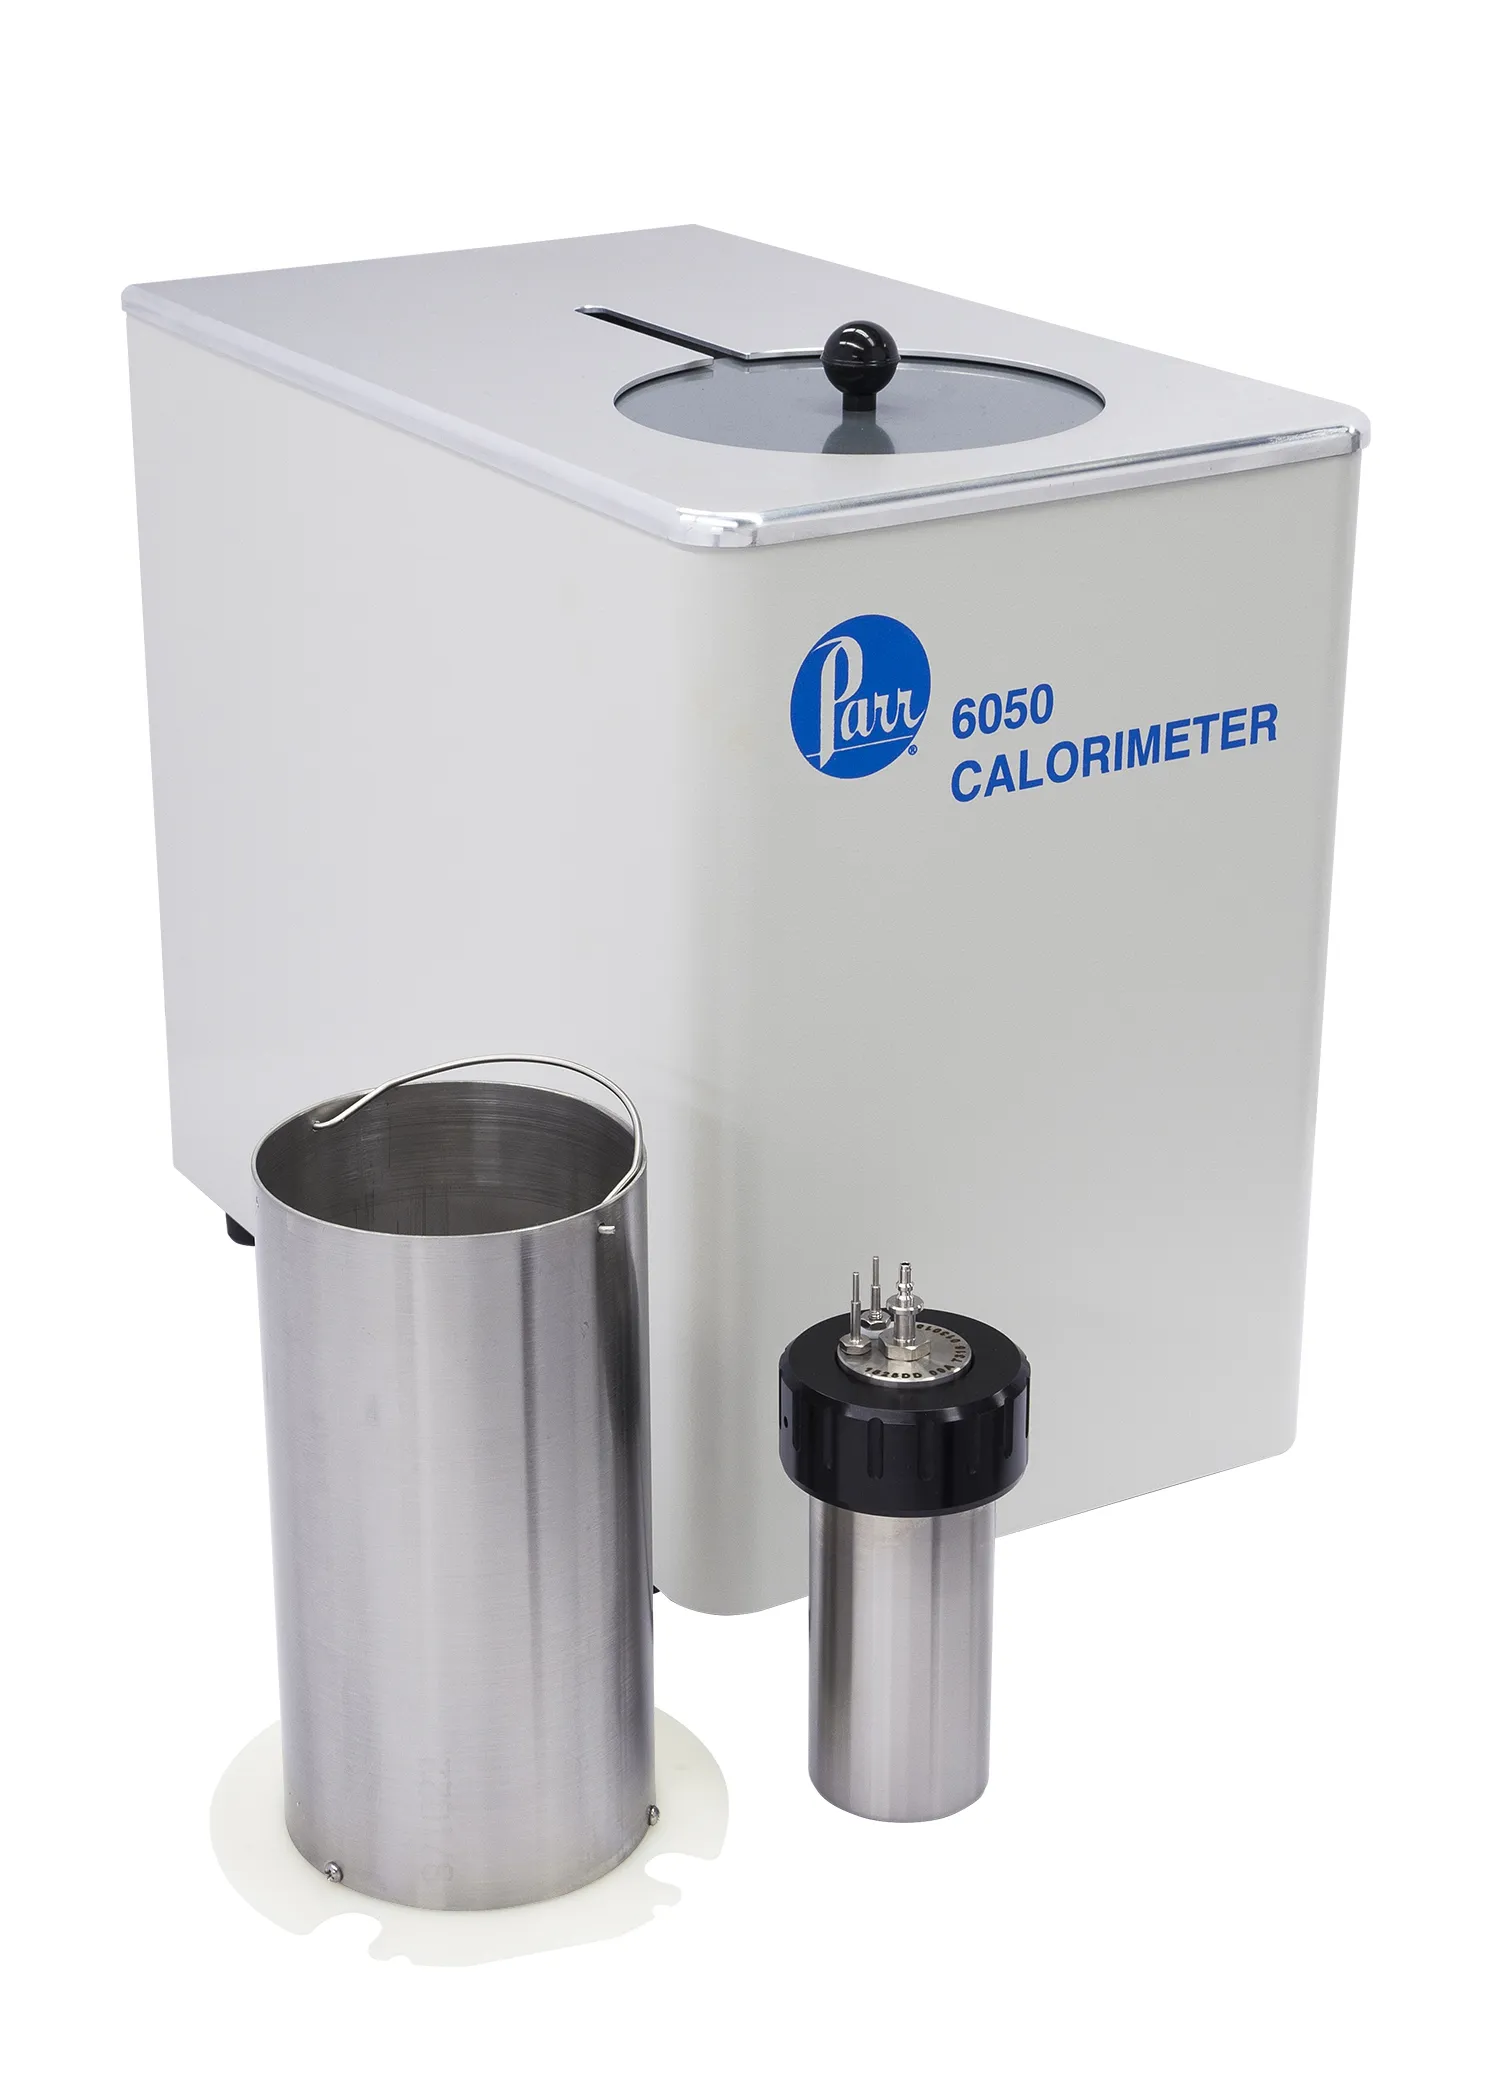
Parr 6050 Compensated Jacket Calorimeter
The oxygen bomb calorimeter is used to accurately measure the heat of combustion of a substance, typically an organic compound such as food, fuel, or polymer.
- Measurement range: typically, up to 10,000 cal/g or more
- Precision: ±0.2% for standard samples
- Analysis time: approximately 10 to 15 minutes per test
- Sample capacity: approximately 0.5 to 1.5 grams

Spectrophotometry equipment
A.1 The Shimadzu model UV-1700 PharmaSep™ spectrophotometer allows the determination of the concentration of a chemical entity in solution, using the Beer-Lambert law. It could be used to determine the percentage of sugars, polyphenols and of proteins. A.2 The Perkins Elmer VICTOR ™ X3™ Plate Reader is a platform for the quantitative detection of light emitting or absorbing markers. The device also includes an improved software package that includes a better start-up wizard, easier protocol creation, temperature control, improved kinetic support for analysis, a stirring system, and an excitation filter wheel, and with 8-position emission.
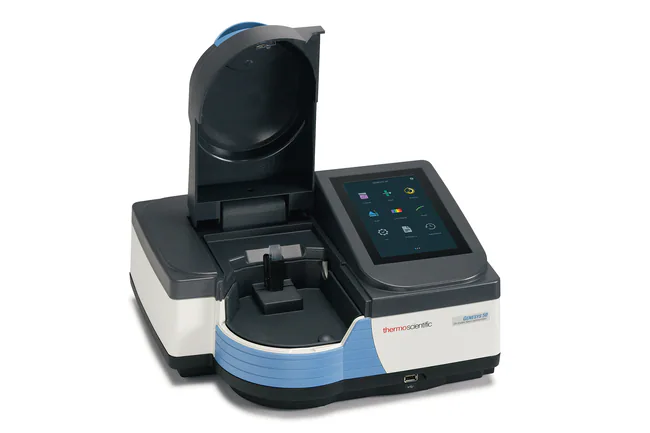
GENESYS™ 50 UV-Visible Spectrophotometer
The GENESYS™ 50 UV-Visible Spectrophotometer is an analytical instrument designed for accurate measurement of absorbance and transmittance in the UV and visible regions. Ideal for compound quantification, reaction monitoring, and material characterization, it serves as an essential tool for research, process development, and quality control applications.
- UV-Visible analysis for absorbance, transmittance, and concentration measurements
- Wide spectral range suitable for research and quality control applications
- User-friendly interface with integrated measurement methods
- High accuracy and excellent reproducibility
- Compatible with a variety of cuvettes and sample holders
- Rapid data acquisition and simplified data processing

Karl Fischer titrator
Mettler Toledo's Karl Fisher C20 titrator™ allows us to determine the amount of water present in a sample. This titrator uses the coulometric method, a titration method in which the titration agent is produced in a solution by electrolysis and the required quantity of the agent is determined by measuring the number of coulombs used to prepare it. The coulometric cell consists of two parts, the anode and the cathode, separated by a diaphragm. The amount of water titrated by the coulometric technique is determined by the amount of Coulomb current used to generate the Iodine. This type of titration is more applicable in the food and petrochemical fields. It can be used for determination of the water content of oils, mineral oils, edible fats and fats.

Viscometer
Viscosity is the resistance to movement of a fluid for flow with or without turbulence. The higher the resistance, the greater the force required to cause this movement, the thicker the substance. The Brookfield™ type viscometer could be used to measure this resistance. The principle of a viscometer is to rotate a needle in a fluid. This viscosity, measured by imposing a speed of rotation, is a dynamic viscosity that is expressed in mPa.s or cPoise This analysis can be used to: control the quality of any fluid; monitor polymerization reactions; control the viscosity of paints. It is applicable in the chemical and petrochemical, food, pharmaceutical industries.

Laboratory scale bioreactor
The BioFlo 110TM is a bench-top fermenter suitable for all levels of research and development. It has an easy-to-use control interface, as well as modules and other accessories to meet various specific needs. It is possible to define setpoints for pH and dissolved oxygen (DO), which can be controlled by addition of a gas, an acid or a base with the cascade function. Two fermenters with a working capacity between 0.4 L and 1 L are available.

Freeze-drying at laboratory scale
The FTS Systems Flexi-Dry FD-1-84A is a compact freeze dryer designed for laboratory-scale freeze-drying applications. Suitable for light to moderate sample volumes, it removes water through sublimation while preserving the structure and properties of heat-sensitive materials. The system is commonly used for sample preservation, analysis, and preparation in research and development environments

Anton Paar Multiwave 3000 (Synthos 3000)
The Anton Paar Multiwave 3000 is a microwave-assisted sample preparation system designed for acid digestion, extraction, leaching, and various sample preparation applications. Featuring advanced temperature and pressure control technology, it ensures fast, safe, and reproducible processing of a wide range of sample matrices. Its versatility and performance make it a valuable tool for environmental, chemical, mining, and industrial laboratories seeking to improve analytical accuracy and efficiency.

Controlled Atmosphere Glove Box (Dri-Lab)
The Dri-Lab glove box is designed for the safe handling of moisture-, oxygen-, and nitrogen-sensitive materials in a highly controlled inert atmosphere. Equipped with a vacuum transfer antechamber and integrated gloves, it enables the preparation, synthesis, and characterization of reactive materials without exposure to ambient air. It is an essential tool for research activities in chemistry, materials science, energy storage, and advanced process development.

Centrifuge CEPA-Z-41
High-speed centrifuge designed for the continuous separation of two liquids or the clarification of liquid-solid mixtures. It can reach a maximum speed of 20,000 rpm, generating a centrifugal force of up to 17,000 g. The cylinder is equipped with a Teflon sheet to optimize the separation process. With a capacity of 2 liters, it offers a minimum flow rate of 20 liters/hour and a maximum flow rate of up to 500 liters/hour, depending on the nature and viscosity of the products being processed. Made of stainless steel, it ensures excellent chemical resistance and superior durability.

Centrifuge Thermo Scientific Modèles Sorvall ST Plus Series
This centrifuge delivers superior performance for a wide range of applications. Centrifugation involves separating the components of a solution with different densities by exposing them to a centrifugal force. This separation process isolates two liquids or separates solid particles from a fluid. The centrifuge offers 9 acceleration profiles and 10 deceleration profiles, allowing the selection of the most appropriate speed profile. Two types of rotors and various adapters are available:
- TX-400 Rotor: Four 400 ml buckets. Conical adapters for 50 ml tubes (maximum capacity of 16 x 50 ml) and conical adapters for 15 ml tubes (maximum capacity of 36 x 15 ml). Maximum speed: 5,000 rpm.
- Fixed-Angle Rotor: Capacity for 6 x 100 ml tubes. Conical adapter for 15 ml tubes (maximum capacity of 6 x 15 ml), conical adapter for 50 ml tubes (maximum capacity of 6 x 50 ml), and adapter for 2 ml tubes (capacity of 16 x 2 ml). Maximum speed: 15,000 rpm / 24,700 g

3900 Series Environmental Chamber
The 3900 series environmental chamber is a device designed to simulate a variety of climatic conditions within a controlled environment. It is ideal for applications such as growth testing, stability studies, and shelf-life evaluations. It allows testing of the resistance of materials, components, or finished products to variations in temperature, humidity, and sometimes other environmental factors. Reliable and versatile, it is well-suited to a wide range of industrial and scientific fields. The chamber features a wide temperature range from 0°C to 60°C, enhancing its operational flexibility. Relative humidity is controlled using a steam generator, allowing levels of up to 95% at 37°C, above ambient temperature.

Silverson L5M-A Emulsifier
Ideal for all laboratory work, research and development, and small-scale production across all industries. Suitable for a wide range of applications—mixing, emulsifying, homogenizing, disintegration, and dissolution—with a level of efficiency and versatility unmatched by other equipment. The system offers a working volume from 1 ml to 12 liters using the same motor base, with the option for inline mixing at flow rates of up to 20 liters per minute. Multiple interchangeable heads are available, equipped with different types of rotor/stator configurations (emulsifying, dispersing, homogenizing).
Typical Applications :
- Production of creams and lotions
- Homogenization of paints or inks
- Dispersion of powders into liquids
- Preparation of nano-emulsions

Jet-O-Mizer 00 Air Jet Micronizer Mill
The Jet-O-Mizer model 00 is a fluid bed jet mill that operates without any moving mechanical parts inside the grinding chamber. It uses high velocity compressed air jets to fracture particles through collision. This mill can grind dry powders to a mean particle size ranging from 0.5 to 45 microns. It is specifically designed for contamination-free milling. The unit is primarily used in the pharmaceutical, chemical, cosmetic, and food industries to achieve very fine particle sizes with a narrow particle size distribution.

Retsch – Heavy-Duty Cutting Mill SM 2000
The Retsch SM 2000 is a heavy-duty cutting mill designed for preliminary size reduction, coarse grinding, and fine grinding of dry, soft, medium-hard, or fibrous materials. It is particularly well-suited for large sample volumes and for use in industrial or laboratory applications. The sieves are easy to change, allowing for flexible adjustment of the final particle size (0.75 µm / 1.0 µm / 1.5 µm / 2.0 mm / 4.0 mm).

LEMITEC MD 80-Sn Decanter Centrifuge
This semi-pilot unit is designed for continuous solid-liquid phase separation on a small scale. Equipped with an integrated screw conveyor system, it enables efficient and continuous separation, even for complex heterogeneous mixtures. It replicates, at laboratory scale, the operating conditions of industrial centrifugal sedimentation processes, while delivering high performance in terms of throughput, clarification speed, and separation accuracy. Its stainless-steel construction, both mechanically robust and chemically inert, ensures excellent chemical resistance and long-term durability. OPERATING PARAMETERS:
- Maximum bowl speed: 10,000 t/min
- Maximum scroll speed: 4,400 t/min
- Product temperature: +5 to +80°C
- Maximum solids concentration : 5% v/v
- Certification : CE
- Processing flow rate: 5 to 100 l/h (depending on the product)
- Filling volume: 220 to 475 mL
- Clarification of sludge or suspensions (organic and inorganic)
- Solid-liquid separation tests for product development and innovation
- Equipment testing before industrial scale-up
- Determination of solid/liquid separation kinetics for complex suspensions
- Evaluation of centrifugation process feasibility
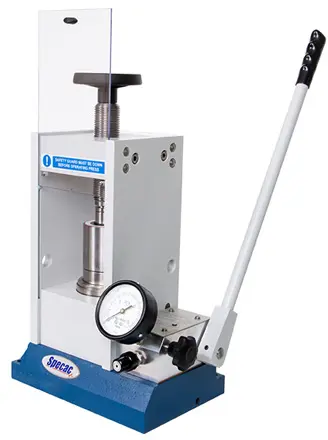
Specac hydraulic press
The Specac hydraulic press is a compact and robust laboratory device designed for the preparation of solid samples. It’s primarily used for forming KBr pellets for infrared spectroscopy (FTIR), compacting powders for X-ray fluorescence (XRF) analysis, and shaping final products into pellet form. Manually operated, it allows precise control of the applied pressure, reaching up to 15 tons—suitable for a wide range of materials. Its construction from durable materials ensures excellent corrosion resistance and long service life.

500 mL High-Pressure Reactor
Designed for research and process development applications, this 500 mL laboratory reactor enables chemical synthesis, process optimization, and feasibility studies at bench scale. Equipped with a mecanic drive stirring system and precise temperature control, it provides safe, reliable, and reproducible operating conditions for a wide range of reactions. Its robust design allows operation under demanding conditions, making it an ideal tool for the development and validation of new products and processes.
- Nominal volume: 500 mL
- Maximum operating temperature: 300°C
- Maximum operating pressure: 35 MPa (350 bar)
- Stirring speed: 0-1000 rpm
- Heating power: 0.6 kW
- Magnetic seal agitation system for enhanced safety and leak-free operation
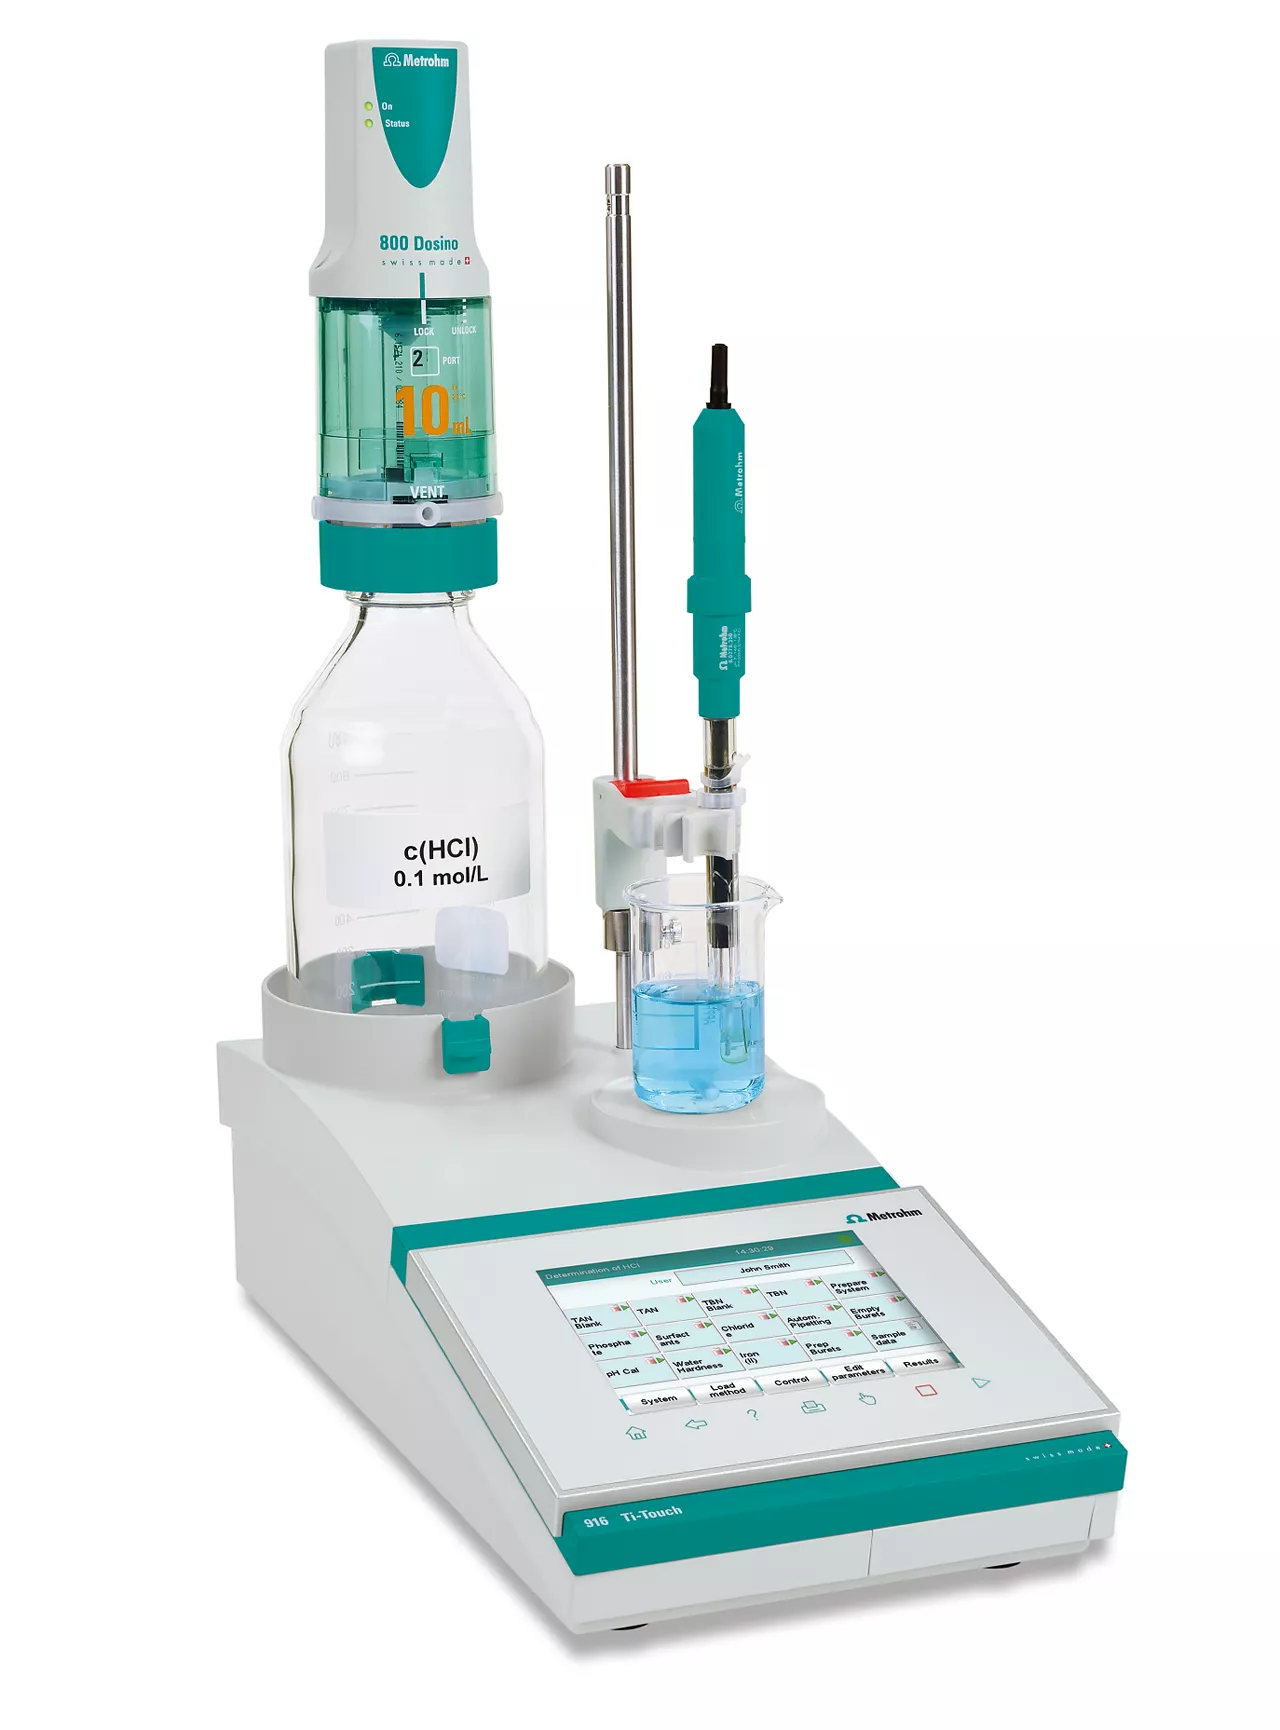
916 Ti Touch titrator
The Metrohm 916 Ti Touch is a compact and automated volumetric titrator designed to deliver both analytical precision and ease of use. Equipped with an intuitive touchscreen, it enables acid-base, redox, complexometric, and precipitation titrations with excellent reproducibility. With its preprogrammed methods and user-friendly interface, it is ideally suited for routine analysis, quality control, and research laboratories. The system features a motorized burette, integrated stirrer, and electrode holder—all in a space-saving design perfect for limited benchtop areas. Applications:
- Acid and base titrations
- Water hardness determination
- Analysis of pharmaceutical, cosmetic, or food products

LabRAM I Acoustic Mixers
The LabRAM I from Resodyn Acoustic Mixers is a benchtop mixer that uses Resonant Acoustic Mixing (RAM) technology. It is designed for research and development as well as small-scale production. The LabRAM operates using high-frequency acoustic waves (60 Hz) that generate intense motion within the containers, ensuring uniform mixing of powders, liquids, pastes, or suspensions—without the need for blades or mechanical agitators. This innovative method significantly reduces mixing time while providing high reproducibility. Compact, quiet, and user-friendly with its touchscreen digital interface, the LabRAM I is especially valued in the pharmaceutical, advanced materials, cosmetics, and specialty chemical sectors for the preparation of complex formulations, dispersions, or homogenizations.
FOX 600 Heat Flow Meter
The FOX 600 Heat Flow Meter from TA Instruments is a thermal conductivity measurement system designed to accurately characterize insulation materials and other low-conductivity products. Compliant with ASTM C518 and ISO 8301 standards, it delivers fast, reliable, and highly reproducible results through advanced heat flow technology, precise temperature control, and digital sample thickness measurement. It is ideally suited for research, development, and quality control applications in the fields of building materials, insulation products, and energy efficiency.
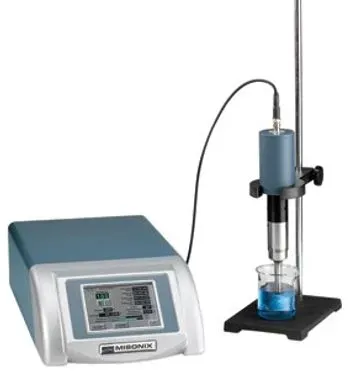
Ultrasonic Processor (Sonicator S-4000)
Designed for advanced laboratory applications, the Sonicator S-4000 uses high-intensity ultrasonic energy to process liquid samples with exceptional efficiency and reproducibility. Operating at 20 kHz, it is ideal for cell disruption, homogenization, nanoparticle dispersion, emulsification, DNA shearing, mixing, degassing, and reaction enhancement. Its digital control system ensures precise adjustment of ultrasonic intensity and process parameters, making it a versatile tool for research and process development.
- Ultrasonic frequency: 20 kHz
- Adjustable amplitude: 1 to 100%
- Universal power supply: 100-240 VAC, 50/60 Hz
- Digital touchscreen interface with programmable operating modes
- Real-time monitoring of power, energy consumption, process time, and temperature (optional probe)
- Compatible with a wide range of probes and accessories for different sample volumes and applications